
Stainless Steel Maintenance Tips for Countertops, Cabinets, and Tables
Most stainless steel maintenance tips reduce to three habits: clean with mild soap and water, dry the surface afterward, and always work along the grain rather than across it. Do that consistently and stainless will outlast almost anything else in the room. The rest of the guidance below covers what to keep off the surface entirely, and how to deal with the marks people actually run into, from water spots to what looks like rust but usually is not.
What Are the Most Important Stainless Steel Maintenance Tips?
Day to day, wipe surfaces with warm water and a small amount of dish soap on a soft cloth or a non-scratch pad, then rinse and dry. Drying is the step people skip, and it is the one that prevents the water spotting and cloudy film that make a surface look neglected.
Weekly, or after heavy use, go over the surface with a cleaner made for stainless steel, applied along the grain and buffed dry. That evens out the finish and removes the film that builds up from cooking oils and hard water.
In a commercial setting, the same routine runs more often rather than differently, and wiping down between services keeps residue from setting.
What Should You Keep Off the Surface of Stainless Steel?
A short list prevents most avoidable damage.
Chlorine bleach and cleaners containing chloride can pit the surface if they are left to sit. If bleach is used, rinse thoroughly and dry rather than letting it evaporate in place.
Steel wool and steel brushes leave behind particles of ordinary steel that rust on your stainless and look like the stainless is failing. Use non-scratch pads instead.
Abrasive powders and scouring cleansers scratch the finish, particularly on polished surfaces.
Salt, citrus, vinegar, and tomato are fine on contact and a problem when left sitting for long periods, so wipe them up rather than leaving them overnight.
Cast iron and other steel cookware left standing on a wet stainless surface transfers material that shows up later as rust-colored spotting.
Common Problems With Stainless Steel
Water Spots and Hard Water Film
Wipe with a solution of equal parts white vinegar and water, then rinse and dry completely. For heavier mineral film, let the vinegar solution sit briefly before wiping along the grain. Drying after every cleaning prevents recurrence better than any product.
Fingerprints
Most common on polished finishes. A stainless cleaner or a small amount of mineral oil applied on a soft cloth and buffed along the grain clears them and slows how quickly they return. If fingerprints are a constant annoyance, a brushed or textured finish hides them far better than polished.
Fine Scratches
Light scratching on a brushed finish usually blends into the grain over time as the surface develops an even patina. For scratches that stand out, a stainless polish or a fine non-woven pad worked strictly along the grain direction can even them out. Deeper scratches are a refinishing job rather than a cleaning one.
Heat Tint and Discoloration
Rainbow or brownish tinting near a heat source is a surface effect, not damage to the metal. A dedicated stainless cleaner or a vinegar solution usually removes it. It tends to return where the same spot gets repeatedly hot, which is normal.
Rust-Colored Spots
Almost always contamination rather than the stainless corroding. Particles from steel wool, cast iron, or nearby grinding land on the surface and rust there. Clean with a non-abrasive stainless cleaner along the grain, and the spots lift without pitting underneath. If spotting keeps returning in the same place, look for the source rather than treating the symptom.
Why Does Working With the Grain Matter?
Brushed and textured finishes have a direction, visible as fine parallel lines. Cleaning along those lines works with the finish. Cleaning across them cuts new lines at an angle, and those catch light differently and never fully blend in. It costs nothing to notice the grain direction before you start, and it is the single easiest way to keep a surface looking consistent for years.
Does Maintenance Differ by Piece?
Countertops take the most direct abuse and benefit most from drying after every cleaning, particularly around sinks and cooktops.
Cabinets mostly need fingerprints and splatter handled, and door faces show wear patterns near handles where hands land repeatedly.
Tables and prep surfaces see cutting, sliding, and impact, so they develop a patina fastest, which is expected rather than a problem.
Outdoor surfaces need periodic washing to clear pollen, dust, and grill residue, plus drying to prevent hard water spotting after rain.
Common Questions About Stainless Steel Care
Can I use glass cleaner on stainless steel?
It works for fingerprints on some finishes, though anything containing ammonia can leave streaks. Mild soap and water followed by drying is the more reliable default.
Will scratches ever come out completely?
Light ones blend in as the surface evens out. Deeper ones can often be reduced by refinishing along the grain, though matching an original factory finish exactly is difficult once a surface has aged.
Is olive oil a good polish?
Mineral oil is the better choice. Cooking oils can go rancid on the surface over time and attract dust.
How do I keep an outdoor stainless surface from spotting?
Dry it after rain or washing where you can, and clean it periodically rather than seasonally. Hard water is the usual culprit, not the steel.
Need a Piece Repaired or Replaced?
Tell us what you have and what happened to it, and we’ll follow up with a clear quote, fast.

The Best Materials for Outdoor Kitchen Cabinets, Compared
The best materials for outdoor kitchen cabinets are the ones that survive water, freezing, and sun without a coating that fails first. In practice that narrows the field to stainless steel, marine-grade polymer, powder-coated aluminum, certain hardwoods, and masonry structures with doors set into them. Each performs differently on cost, appearance, and how much attention it needs over ten years. Below is what each one actually does in a climate with real winters, including where each falls short.
What Are Outdoor Cabinets Up Against in a Wisconsin Climate?
Four forces do the damage. Moisture works into anything porous. Freeze-thaw cycling expands that trapped water and pries materials apart across a winter. Ultraviolet light breaks down finishes, sealers, and plastics. And pests chew into anything soft enough to nest in.
A material that handles three of those and fails at the fourth still fails. That is the standard to judge each option against.
What Are the Best Materials for Outdoor Kitchen Cabinets?
Stainless Steel
Very well, which is why it is the default in most outdoor kitchens. It does not absorb water, has no coating to peel, is unaffected by UV, and gives pests nothing to chew. It can be fabricated to any dimension, so it fits around equipment and existing structure.
The tradeoffs: it is typically the highest material cost, it shows water spots and fingerprints on polished finishes, and it heats up in direct sun. Lower grades can show surface spotting in wet or lakeside conditions, so grade selection matters more here than indoors.
Marine-Grade Polymer?
A high-density plastic that handles water and UV well, comes in colors, stays cool to the touch, and needs almost no maintenance. It is a legitimate option and a common one.
The tradeoffs: it can expand and contract with temperature more than metal, heavy doors can sag over long spans, colors can fade over many years, and it reads as plastic up close, which matters to some homeowners and not at all to others.
Powder-Coated Aluminum
Light, corrosion-resistant, available in colors, and less expensive than stainless. For many outdoor kitchens it is a sound middle option.
The tradeoff is the coating. Powder coat is durable but it is still a layer, and once it chips or is scratched through, the damage is visible and the repair is a touch-up rather than a polish. Sustained sun exposure fades some colors over time.
Teak and Other Hardwoods
They can, and nothing else looks like them. Teak, ipe, and similar dense hardwoods have natural oils that resist rot and insects, and a well-made hardwood outdoor kitchen is genuinely beautiful.
The tradeoff is attention. Wood moves with humidity, weathers to gray without regular oiling, and needs refinishing on a cycle. In a freeze-thaw climate that maintenance is not optional if you want it to look new. Budget the upkeep honestly before choosing it.
Masonry and Stone-Clad Structures
Block, stone, or stucco structures are permanent and handle weather indefinitely. Most masonry outdoor kitchens are really a hybrid, since the doors and drawers set into the structure are metal or polymer.
The tradeoffs: it is the least flexible option once poured, the most expensive to change, and it requires a proper footing in a climate that heaves. Interior storage also stays cooler and damper than a metal box, so ventilation matters.
Why Doesn’t Indoor Cabinetry Work Outside?
Because every component is wrong for the conditions. Particleboard and MDF swell. Plywood delaminates. Laminate peels from behind. Hinges and slides that are not rated for outdoor use seize or corrode within a season or two. Covering an indoor cabinet with an outdoor-rated finish delays the failure rather than preventing it.
Which Material Matches Your Priority?
If budget leads, powder-coated aluminum or marine polymer gives you the most durable result per dollar.
If low maintenance leads, stainless steel and marine polymer both ask very little of you.
If appearance leads, the answer depends on the look. Hardwood for warmth, stainless for a clean modern line, masonry with metal doors for something that reads as part of the architecture.
If longevity leads, stainless steel and masonry outlast the rest, particularly through repeated hard freezes.
Where Do These Materials Get Mixed?
Constantly, and it is usually the right call. A masonry structure with stainless doors and drawers is one of the most common outdoor kitchen configurations, because the stone carries the look and the metal carries the working parts. Stainless cabinets under a hardwood-clad island is another. Choosing one material for the whole kitchen is rarely necessary and often more expensive than the hybrid.
Common Questions About Outdoor Kitchen Cabinet Materials
Which material lasts the longest outdoors?
Stainless steel and masonry, with the caveat that stainless grade and masonry footing both affect the answer. Neither depends on a coating that can fail.
Can outdoor cabinets stay outside through a Wisconsin winter?
Materials rated for outdoor use can. The bigger winter issues are usually plumbing and appliances rather than the cabinet boxes, so plan for winterizing whatever holds water.
Do I need to cover an outdoor kitchen?
Covers extend the life of every material and are worth using, though a properly specified outdoor kitchen should not depend on one to survive.
Can I mix materials without it looking mismatched?
Yes, and most well-designed outdoor kitchens do. Consistency in finish and hardware carries the look further than using a single material everywhere.
Planning an Outdoor Kitchen?
Send us your layout and appliance list, and we’ll follow up with a clear quote, fast.
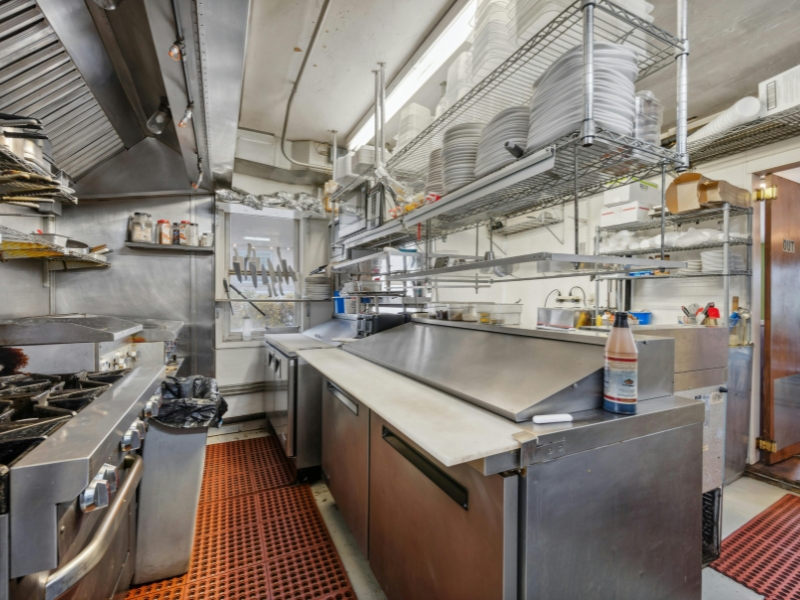
Why Stainless Steel Is Used in Commercial Kitchens
Why stainless steel is used in commercial kitchens comes down to a surface that absorbs nothing, tolerates heat, survives industrial cleaning chemicals, and can be repaired instead of replaced. A working kitchen puts more stress on its surfaces in a year than a home kitchen does in a decade, and most materials that look fine in a showroom cannot take it. Stainless can, which is why it became the standard long before it became a design choice.
What Is a Commercial Kitchen Doing to Its Surfaces?
It helps to be specific about the abuse, because that is what the material selection is answering.
Heat arrives constantly, from pans set down straight off a burner and from equipment radiating all service. Moisture never fully leaves, between washdowns, steam, and splash. Cleaning chemicals are far more aggressive than anything used at home, applied several times a day. Volume means hundreds of contacts per surface per shift. And impact happens, because full hotel pans and stock pots get set down hard by people moving fast.
Any surface in that room is being tested on five fronts at once, every day, for years.
Why is Stainless Steel Is Used in Commercial Kitchens Rather Than the Alternatives?
Nonporous
It means there is no structure in the surface for liquid or residue to enter. Raw protein juices, oil, acid from citrus and tomato, and cleaning solution all stay on top of the metal until they are wiped away. Porous surfaces need a sealer to imitate that, and a sealer is a consumable that degrades with heat and chemicals. Stainless has no layer to lose.
Heat Tolerance
More than a kitchen produces. Hot pans set directly on a stainless surface do not scorch it, discolor it permanently, or weaken it. Surfaces next to fryers and ranges hold their shape through years of thermal cycling, which is where laminates delaminate and sealed stone develops cracks near seams.
Commercial Cleaning Chemicals
Yes, which is a bigger deal than it sounds. Degreasers and sanitizers used in food service are far harsher than household cleaners, and they are applied constantly. Stainless tolerates that routine without the surface breaking down. The main exception is chlorine bleach left sitting, which can pit the surface and should be rinsed rather than allowed to dry.
Damage
It can usually be repaired in place. Scratches blend into a brushed finish or can be worked back along the grain. A dented section can be replaced without tearing out the run beside it. A worn edge can be re-welded and polished. Compare that to a chipped stone counter or a delaminated laminate top, where the practical answer is replacement.
What Does “Stainless” Actually Mean?
It is an alloy, not a coating. Chromium in the steel reacts with oxygen to form a thin passive layer across the surface, and that layer is what resists corrosion. The useful part is that it reforms on its own when the surface is scratched, so a scuff does not create a permanent weak spot the way a break in a coating does.
Stainless resists rust rather than being immune to it. Most rust-colored spotting people find on a stainless surface is contamination from another metal left sitting there, such as a steel wool pad or a cast iron pan, and it cleans off without the stainless underneath being affected.
Where Does Fabrication Quality Show Up?
The material only delivers if the piece is made well, and this is where kitchens differ most.
Welded seams that are ground and polished smooth leave nothing to trap residue. Coved corners are easier to clean than square internal corners. Surfaces sloped toward a drain clear water instead of holding it. Edges that turn down rather than ending in a raw cut are safer and hold their shape. Pieces fabricated to the room’s real dimensions close the gaps where standard equipment leaves an unreachable strip along a wall.
Two kitchens can be built from the same material and clean very differently depending on how the pieces were fabricated.
What Doesn’t Stainless Steel Solve?
It scratches, and in a commercial kitchen it will, quickly. The finish develops a working patina within months, which is normal and does not affect performance. It shows water spots in hard water areas unless surfaces are dried. It dents under heavy impact. And it does nothing about a poor layout, because the best surface in the world still fails if the station it sits in makes people reach across a hot line.
Common Questions About Stainless Steel in Commercial Kitchens
Does stainless steel harbor bacteria?
The surface is nonporous, so there is nowhere for residue to soak in, which is why it is the standard for food contact surfaces. Cleaning practice still does the real work, and seam and corner quality affects how easy that is.
Why do some kitchens have stainless that looks worse than others?
Usually a combination of finish choice, water hardness, and cleaning method. Abrasive pads used across the grain and chlorine cleaners left to dry account for most of the damage people blame on the metal.
Is thicker stainless always better?
Heavier material resists denting and feels more solid, and it costs more. The right choice depends on the piece, since a prep table takes different abuse than a wall panel.
Can stainless surfaces be added to a kitchen that is already running?
Yes. Individual pieces can be fabricated to match existing dimensions and finish and installed around service hours, which is far easier than replacing a full run.
Outfitting a Commercial Kitchen?
Send us your layout and equipment list, and we’ll follow up with a clear quote, fast.

Custom Metal Fabrication for Restaurants, Zone by Zone
Custom metal fabrication for restaurants covers nearly every working surface between the back door and the bar. Prep tables, countertops, backsplashes, shelving, cabinets, and equipment stands all get fabricated to the dimensions of your actual space rather than ordered in standard widths and made to fit. The reason to go custom is not appearance. It is that a commercial kitchen is a workflow, and standard sizing forces compromises in exactly the places where a few inches change how a shift runs.
What Does Custom Metal Fabrication for Restaurants Cover, Zone by Zone?
Following the path food takes through the space is the easiest way to scope a project.
Receiving and Dry Storage
Heavy-duty shelving sized to the room rather than to a catalog, wall-mounted racks that clear a door swing, and rolling carts built for the aisle width you actually have. This zone is where standard shelving wastes the most space, because storage rooms are rarely dimensioned like showroom displays.
Prep Area
Prep tables sized to the crew that works them, with undershelves at heights that match your containers. Wall-mounted shelving above. Sink assemblies with integrated drainboards. This is the zone where custom sizing pays off fastest, because prep stations are where people stand shoulder to shoulder during a rush.
Cook Line
Equipment stands sized to the specific pieces you bought, landing shelves at the pass, and backsplashes and wall panels behind the line where grease and heat hit hardest. Cook lines are almost never a clean rectangle, and the gaps standard equipment leaves are the hardest places in a kitchen to keep clean.
Dish and Warewashing?
Soiled and clean landing tables sized to your machine, sloped surfaces that drain where you want them to, and wall panels around the splash zone. Dish is the wettest area in the kitchen, which makes seam quality and drainage more than a cosmetic concern.
Front of House and Bar
Bar tops, speed rail structures, back-bar shelving, service counters, and stations sized around the ice bin and glass washer you already own. Front-of-house work has to survive the same abuse as the back while looking like part of the dining room.
Why Does Custom Sizing Beat Standard Equipment in a Restaurant?
Standard commercial equipment comes in fixed widths. Real kitchens come in whatever dimensions the building gave you, usually with a column, a floor drain, or a door in an inconvenient spot.
Filling the difference with a gap creates a place that collects debris and cannot be cleaned properly. Filling it with a piece of trim creates a seam that fails. Fabricating the piece to the actual dimension removes the problem instead of covering it, and it recovers working surface you would otherwise lose in half-inch increments across the room.
How Does Fabrication Fit a Restaurant Timeline?
Restaurant projects run against fixed dates. An opening, a lease start, an inspection, a reopening after a remodel. Kitchen fabrication tends to land late in the sequence, after the space is framed and the equipment is specified, which compresses the window.
The practical move is getting measurements taken as early as the space allows and confirming the equipment list before fabrication starts, since a change to one appliance can change the dimensions of the pieces on both sides of it. Tell your fabricator the opening date at the quote stage rather than after the order, so anything unrealistic surfaces while there is still time to adjust.
Can You Work Alongside Our Contractor or Kitchen Designer?
That is the normal arrangement rather than the exception. On most buildouts the fabricator coordinates with a general contractor on wall and utility locations, with a kitchen designer on layout, and with the equipment supplier on final appliance dimensions.
What makes that go smoothly is early access for field measurements and a confirmed equipment list. What makes it go badly is fabricating from architectural drawings that never got updated after a wall moved.
Can Pieces Be Replaced in a Kitchen That’s Already Open?
Yes, and it is common. A worn prep table, a damaged countertop, a backsplash behind a replaced piece of equipment, or a new station added to an existing line can all be fabricated to match what is already there.
The advantage over ordering a replacement is fit. A piece made to the current opening drops in without shimming, and it can be scheduled around your service hours rather than requiring a shutdown.
Common Questions About Restaurant Fabrication
How early should we start the fabrication conversation?
As soon as you have a layout and an equipment list, even a draft one. Early conversations are cheap, and late changes are not.
Can you match existing pieces in our kitchen?
Usually. Matching finish and dimension on an existing run is routine, which is often easier than sourcing a discontinued equipment line.
Do you handle installation?
Ask about delivery and installation support when you request a quote, since coordination around your schedule is part of the scope on most restaurant work.
What should we send to get a quote?
A kitchen layout, your equipment list with model numbers, your target date, and photos of the space if it exists yet. That combination gets you a real number rather than a range.
Have a Kitchen Timeline to Hit?
Send us your layout and opening date, and we’ll follow up with a clear quote for your kitchen, fast.

How to Choose a Metal Fabrication Company
How to choose a metal fabrication company comes down to a handful of questions you can ask any shop before you send a drawing. What can they do under their own roof? How does work get inspected before it ships? Who picks up the phone when something goes wrong? Are their timelines real? The shops that answer those clearly tend to be the ones that deliver, and the ones that answer vaguely tend to be the ones you end up chasing. Here is what to ask and why each answer matters.
What Can They Actually Do In-House?
This is the first filter, and it explains more about your future experience than any other single answer. A shop that cuts, forms, machines, welds, and assembles under one roof controls its own schedule. A shop that subcontracts half of that is coordinating other people’s queues, and every handoff is a place where your timeline can slip without anyone telling you.
Ask specifically which operations occur on-site and which are sent out. Then ask what happens to your lead time when a subcontracted step gets delayed. The answer tells you how much of the schedule they actually control.
How Does Work Get Inspected?
Every shop will say quality matters. The useful question is mechanical: at what points in the process does someone check the part against the drawing, and what happens when a dimension is out?
You are listening for a described process rather than a reassurance. Inspection at defined stages, checks against your original drawing, and a stated path for what happens when something does not measure right. A shop that can walk you through that has thought about it. A shop that says everything gets checked has not.
Who Will You Talk to When Something Goes Wrong?
Something will. A drawing will have an ambiguity, a material will be back-ordered, or a dimension will need a decision that nobody anticipated. What separates vendors is not whether problems happen but how fast you hear about them.
Ask who your point of contact is, whether that person can reach the floor directly, and how quickly you would find out if your job hit a snag. The worst outcome is not a delay. It is a delay you learn about on the day the part was supposed to arrive.
Are Their Timelines Realistic, and What Happens When One Slips?
A shop that agrees to every date without hesitation is either very well equipped or not being straight with you. The better sign is a shop that asks about your deadline early, tells you when it looks tight, and proposes what would have to change to hit it.
Ask how they handle a rush job, because the answer reveals capacity. A shop with real flexibility can describe how work gets prioritized. A shop without it will say yes and hope.
Can They Show You Work They’ve Already Done?
Photos of finished projects, examples in your industry, and a willingness to talk through how a specific job was approached all carry more weight than a capabilities list. You are looking for evidence they have solved a problem shaped like yours.
If your project is unusual, ask directly whether they have done something comparable and what was difficult about it. The specificity of the answer is the signal.
How Much Should Location Matter?
More than most buyers weigh it initially. A nearby shop means you can visit the floor, drop off a sample, or pick up a part the same day when a line is down. It means shipping is not a variable in your lead time. And it means accountability is face to face rather than through a portal.
For manufacturers running production, that proximity often turns out to be the deciding factor after the first urgent job.
How to Choose a Metal Fabrication Company You’ll Use Again
The shops worth keeping are the ones that behave the same on the fifth order as on the first. Consistent quality, honest dates, and a phone call when something changes. Those are not glamorous criteria, and they are exactly what people mean when they say they have finally found a good fabricator.
Run a small job first if you can. One real order teaches you more about a shop than any number of conversations.
Common Questions About Choosing a Fabrication Shop
Should I pick the lowest quote?
Not on its own. Compare what each quote includes, since finishing, inspection, and delivery are sometimes priced in and sometimes not. A low number with steps missing is not actually lower.
What should I send to get an accurate quote?
Drawings or a 3D model, material and thickness, quantity, finish requirements, timeline, and where the part will be used. Missing details are the most common reason a quote comes back with caveats.
Does a shop need to be certified?
It depends on your industry and your own requirements. Ask what certifications a shop holds and whether they are relevant to your part rather than treating any certificate as a general quality score.
How do I evaluate a shop for ongoing production rather than one job?
Ask about capacity, repeatability across runs, how they handle revisions, and what happens when your volume changes. Production relationships fail on consistency far more often than on capability.
Looking for a Fabrication Partner?
Send us your drawing and your timeline, and we’ll follow up with a clear quote and a straight answer on the date, fast.
Design for Manufacturability: How to Design Metal Parts That Are Easier to Fabricate
Design for manufacturability means drawing a part so it can be made efficiently with the processes that will actually make it. The same function can often be delivered two ways, one of which costs noticeably more to produce, and the difference is usually decided on the drawing rather than on the shop floor. Tolerances tighter than the part needs, holes placed too close to a bend, a joint no welder can reach, and material chosen against the process account for most avoidable cost in fabricated parts.
What Makes a Part Expensive to Fabricate?
Rarely the thing people expect. Raw material is often a minor share of the total on a fabricated part. What drives cost is operations, setups, and risk.
Every additional process step adds handling. Every repositioning in a fixture adds a setup. Every tolerance tight enough to require inspection adds time and scrap exposure. A part that looks simple can carry six operations, and a part that looks complex can carry two. Counting operations rather than judging appearance is the useful instinct.
Are Your Tolerances Tighter Than They Need to Be?
This is the single largest source of unnecessary cost, and it usually comes from caution rather than requirement. A tolerance copied from a template, or tightened because it felt safer, quietly commits the shop to slower processes and added inspection on features where nothing was ever at stake.
The productive habit is asking, feature by feature, what the tolerance is protecting. A hole that clears a bolt does not need the tolerance of a hole that locates a bearing. Tighten what matters functionally and open up everything else. A drawing where a few features are tight and the rest are general tells a shop exactly where to spend attention.
Where Should Bends and Holes Sit Relative to Each Other?
Metal stretches on the outside of a bend, so a hole placed too close to a bend line distorts into an oval as the part is formed. The part measures correctly flat and wrong afterward, which is a frustrating way to discover the issue.
Moving the hole away from the bend solves it. If the hole has to stay where it is, the alternative is forming first and cutting the hole afterward, which adds an operation. Flanges that are too short to clamp create a similar problem, since a press brake needs enough material to hold. Bends running very close to each other can also conflict, because the tooling and the already-formed portion of the part need somewhere to go.
Can a Welder Physically Reach That Joint?
Access is the constraint most often missed in CAD, where a model can be assembled in an order no human hand could follow. A joint inside a closed box, a weld behind a flange, or a seam accessible only after another component blocks it all look fine on screen.
Two questions catch most of it. Can a torch reach this joint at a workable angle, and can the assembly be held in position while it is welded? Adding an access opening, splitting a component, or changing assembly order usually costs far less than the workaround required when the part arrives unweldable. It is also worth asking whether the weld is needed at all, since a single formed piece frequently replaces several welded ones.
Does the Material Choice Fight the Process?
Sometimes, and it shows up late. Material that work-hardens as it is formed behaves differently than material that does not. Springback varies by alloy, so a bend angle correct in one material needs different setup in another. Minimum bend radius depends on thickness and material together, and specifying a tighter radius than the material accepts cracks the outside of the bend.
Grain direction matters too, since bending parallel to the grain is harder on the material than bending across it. None of this requires a metallurgy background. It requires naming the material and thickness early enough that the process can be checked against it.
What Can You Standardize to Cut Cost?
Repetition is cheaper than variety, and most drawings carry more variety than the design requires.
Use one material thickness across an assembly where you can, rather than three that each need their own setup. Use a consistent hole size for fasteners of the same type, so one tool does the work. Use consistent bend radii, since each distinct radius may call for different tooling. Reuse a proven geometry rather than drawing a new one for a part doing the same job as an existing piece.
None of these change what the part does. All of them reduce what it takes to make it.
When Does Design for Manufacturability Save the Most Money?
Before the drawing is finalized, which is the part that gets skipped. Once a design is approved and released, changing it means revision cycles, re-approvals, and sometimes re-quoting, so the easy savings have already hardened into commitments.
A short review while the design is still soft costs almost nothing. A fabricator looking at a draft can flag the three features driving most of the cost, and in a lot of cases the fix is moving a hole, opening a tolerance, or changing a thickness. That is the whole argument for involving the shop early rather than sending a finished package and hoping.
Common Questions About Design for Manufacturability
Do I need a finished drawing to start the conversation?
No, and earlier is better. A sketch with dimensions and a description of what the part does is enough to catch the expensive decisions while they are still easy to change.
Will simplifying a design compromise the part?
It should not. The goal is removing requirements that were never functional, not weakening ones that are. Anything load-bearing or dimensionally critical stays where it needs to be.
Does this apply to one-off parts or only production runs?
Both, though the payoff scales with quantity. On a single part, the savings are usually in setups. On a production run, small per-part savings multiply.
What file formats are most useful?
A 3D model plus a dimensioned drawing covers most cases, with DXF for flat profiles. Send what you have rather than waiting until the package is complete.
Have a Design in Progress?
Send us your drawing or sketch, and we’ll flag what drives the cost before you finalize it.

What Is Press Brake Forming?
What is press brake forming? It is the process that turns a flat piece of sheet metal into a part with angles in it. A machine called a press brake clamps the sheet between a punch above and a die below, then presses the two together so the metal bends along a straight line. Repeat that a few times in the right places and a flat blank becomes a bracket, an enclosure, a channel, or a panel. Almost every fabricated metal part with a bend in it went through this step.
What Is Press Brake Forming Doing to the Metal?
The punch pushes the sheet down into the die, and the metal bends around the shape of the tooling. The outside of the bend stretches slightly and the inside compresses, which is why every bend has a radius rather than a sharp corner. That radius is a real dimension, not a rounding error, and it affects the finished size of the part.
Metal also has memory. When the pressure releases, the material springs back a little toward flat. Forming accounts for that by overbending slightly, and how much depends on the material and its thickness. This is why the same drawing bent in aluminum and in stainless needs different setups to land on the same angle.
What Parts Come Off a Press Brake?
More than most people expect. Mounting brackets and angle pieces. Enclosures and electrical boxes. Machine guards and panels. Structural channels and hat sections. Trays, pans, chutes, and hoppers. Countertop and cabinet edges that turn down or fold back on themselves. Anything with a flange, a lip, or a right angle that started life as flat stock.
Formed parts often replace welded assemblies. A single piece bent into a U shape is faster, cleaner, and stronger than three flat pieces welded together, which is why forming shows up early in the design of a well-made part.
Where Does Forming Fit in the Fabrication Sequence?
Usually second. The flat shape gets cut first, on a laser or a water jet, with hole locations and the outer profile already in place. Then the part is formed. Then it gets welded, machined, or assembled as the job requires.
That order matters, because holes and features are far easier to locate accurately on a flat sheet than on a part that has already been bent. It also means the flat pattern has to be drawn with the bends in mind, since the material consumed by each bend changes how big the blank needs to be.
What Affects Whether a Bend Comes Out Right?
Material and Thickness
Different metals bend differently. Stainless takes more force and hardens as it is worked. Aluminum bends easily but springs back more. Thickness changes the minimum radius the material will accept without cracking on the outside of the bend.
Bend Radius
Every bend has one, and specifying an unrealistically tight radius for the material and thickness is one of the more common issues on drawings. If a radius is not called out, the shop will use what the tooling and material support.
Grain Direction
Rolled sheet has a grain. Bending across it is more forgiving than bending along it, particularly on tighter radii, where bending parallel to the grain can crack the outside of the bend.
Hole and Feature Placement
Holes placed too close to a bend line distort as the metal stretches. Moving them a small distance away, or forming first and drilling after, avoids a part that measures fine on the flat and wrong once bent.
What Should You Send When You Request a Quote?
A drawing or DXF is the starting point, with the material and thickness called out. Bend angles and flange dimensions should be on it, along with any radius requirement you actually need held. Quantity matters, because setup cost spreads differently across one part than across two hundred.
If you have a 3D model, send that too. If you only have a sketch and a description of what the part has to do, that is still workable, and forming is one of the areas where a short conversation early saves a revision later.
Common Questions About Press Brake Forming
Is press brake forming the same as bending?
Bending is what happens, and press brake forming is how it happens. Roll forming, tube bending, and hand brakes all bend metal too. A press brake does it with a punch and die, which gives repeatable angles across a run of parts.
Can you form a part after it has been welded?
Sometimes, though it is usually harder and less accurate. Forming before welding is the normal sequence for good reason.
How tight can a bend be?
It depends on the material, the thickness, and the tooling. Every material has a point where the outside of a bend cracks rather than stretches. Send the drawing and we will confirm what your material supports.
Do you form one-off parts or only production runs?
Both. A single prototype and a full production order run through the same process. Quantity changes the per-part price, not whether the job is worth doing.
Have a Part to Form?
Send us your drawing or DXF, and we’ll follow up with a clear quote for press brake forming, fast.
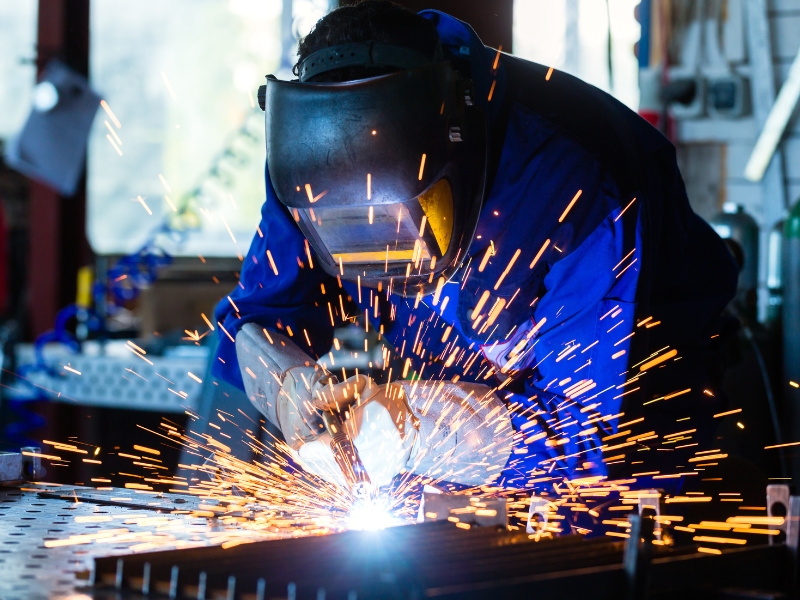
MIG Welding vs. TIG Welding: What’s the Difference?
The short version of MIG welding vs TIG welding: MIG feeds a wire continuously and lays down metal fast, while TIG uses a non-consumable tungsten electrode and gives the welder precise control over a much smaller, cleaner weld. MIG is quicker and better suited to production work and thicker material. TIG is slower, more controlled, and the choice when the weld will be visible or the material is thin. Most shops run both, because most projects have some of each.
How Does MIG Welding Work?
A MIG gun feeds a spool of wire through the torch and into the joint while shielding gas protects the weld pool from the air. The wire is both the electrode and the filler, so the welder can keep moving without stopping to add material.
That continuous feed is what makes MIG fast. It deposits metal quickly, handles longer runs without interruption, and is more forgiving of variation in fit-up. On structural work, brackets, frames, enclosures, and anything where the weld will be ground, painted, or hidden, that speed translates directly into cost.
How Does TIG Welding Work?
TIG uses a tungsten electrode that does not melt into the weld. The arc heats the material, and the welder adds filler rod separately by hand, one dab at a time, while controlling heat input with a foot pedal or torch control.
Separating the heat source from the filler is the whole advantage. The welder controls exactly how much heat goes in and exactly how much metal is added, which produces a narrow, precise, clean weld with very little spatter. It is slower by nature, because control and speed are trading against each other.
What Do You Actually Notice in MIG Welding vs TIG Welding?
Appearance
TIG produces the stacked-dime bead people picture when they think of an attractive weld, with little spatter and minimal cleanup. MIG beads are wider and typically leave some spatter to clean up. If the weld will be seen on a finished product, that difference drives the decision on its own.
Price
MIG, clearly, on most work. Continuous wire feed and higher deposition mean fewer hours in the same joint. On a long run of structural welding, the difference is substantial. TIG costs more per inch of weld because it takes more time per inch.
Materials
MIG handles mild steel and stainless well and works on aluminum with the right setup. TIG handles stainless, aluminum, and thinner or more sensitive materials with more control, and it is the usual answer when the material is unforgiving or the joint is small.
Thickness
TIG, without much argument. Fine heat control is what keeps thin sheet from burning through or distorting. MIG puts more heat in faster, which is an advantage on heavy material and a liability on light gauge.
Which One Does Your Project Need?
Ask what the weld has to do. If it has to hold, be produced efficiently, and end up hidden or finished over, MIG is usually right. If it has to look good in the final product, sit on thin material, or hold tight distortion control, TIG earns its extra time.
For custom stainless work that will be seen, such as a countertop seam, a railing, or an exposed frame, TIG is generally the answer. For a run of brackets that get powder coated, MIG almost always is.
Why Would a Shop Use Both on One Job?
Because most assemblies have a mix of joints. The hidden structural welds inside a frame do not need the appearance of the visible seam on the outside, and paying for TIG time on both is wasted money. Choosing process by joint rather than by job is common practice, and it keeps cost down without giving up the finish where it matters.
Common Questions About MIG Welding vs TIG Welding
Is one stronger than the other?
A properly executed weld in either process can be plenty strong. Strength comes from joint design, fit-up, penetration, and welder skill far more than from which process was chosen.
Is TIG always better?
No. It is more controlled and better looking, and it costs more time. On a joint that will never be seen, that spend buys nothing you can use.
Which process should I ask for on a quote?
Describe what the finished part needs to look like and where it will be used, and let the shop recommend the process. Specifying it yourself can raise the price without improving the result.
Can both processes be used on stainless steel?
Yes. Both weld stainless routinely. TIG is more common where the weld stays visible, and post-weld finishing matters either way for both appearance and corrosion resistance.
Have a Welding Project?
Tell us what the part is and where the welds will be seen, and we’ll follow up with a clear quote, fast.
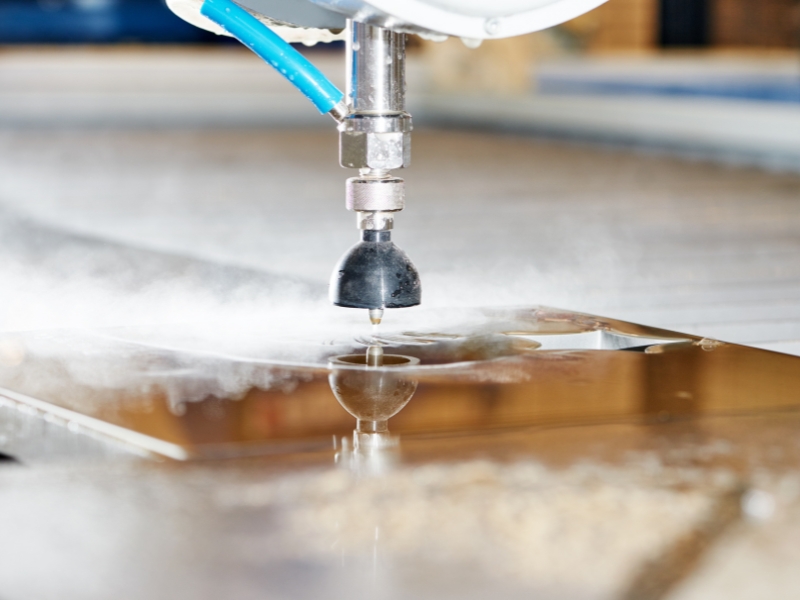
When to Use Water Jet Cutting for Metal Fabrication
Knowing when to use water jet cutting comes down to reading a few signals in your own drawing. The process cuts with pressurized water and abrasive rather than heat, so it earns its place whenever heat would damage the part, the material is thick, the geometry is complicated, or the job involves something other than sheet metal. On thin steel in high volume, another process is usually faster and cheaper. Here is how to tell which situation you are in before you request a quote.
When to Use Water Jet Cutting: What You Should Look for in Your Drawing
Five things push a job toward water jet, and most parts that belong there show at least two of them. Run through your drawing and see how many apply.
Does Your Part Need to Stay Cool?
This is the strongest signal. Water jet cutting is a cold process, so there is no heat-affected zone along the edge and no change to the temper, hardness, or grain structure of the material next to the cut.
That matters on hardened and heat-treated material, where a thermal process can undo the treatment right where the part is most likely to be loaded. It matters on parts with critical requirements near the cut edge. And it matters on plastics, composites, and laminates that melt, char, or delaminate under heat. If your material was heat-treated on purpose, cutting it cold protects the work already done.
Is the Geometry Complicated?
Water jet cutting follows intricate profiles without tool wear changing the result partway through a run. Interior cutouts, tight radii, sharp interior corners, and nested shapes all cut cleanly, and the tenth part matches the first. There is no tooling to make, which is why one-off and short-run work with complex outlines often lands here even when the material would be easy to cut another way.
Is the Material Thick?
Thermal cutting processes lose speed and edge quality as material gets heavier. Water jet slows down as well, but the edge stays consistent, so on heavy plate it frequently becomes the practical choice even when another process could technically make the cut. If your part is plate rather than sheet, water jet is worth pricing.
Does the Job Involve More Than One Material?
Water jet cutting is close to material-agnostic. Stainless, aluminum, mild steel, copper, titanium, stone, glass, composite, rubber, and foam all run on the same machine. When a project includes gaskets alongside metal parts, or a stone or composite element next to a fabricated bracket, consolidating those cuts onto one process removes a vendor and a handoff from the schedule.
Does the Edge Need to Be Clean Off the Machine?
Water jet leaves a matte, sandblasted edge with very little burr, which often means no deburring step at all. On parts where secondary finishing would otherwise eat labor hours, that changes the total cost even when the cutting itself is slower. For stainless work in particular, an edge that needs no rework is worth quoting against a faster process that does.
Which Process is Right For You?
Being straight about this makes the rest of the guidance more useful. Water jet is not the answer for thin sheet metal in production volume, where thermal cutting is meaningfully faster and cheaper per part. It is not the answer when the part is simple, the material is ordinary, and quantity is high. And it is not the answer when a formed or machined feature would be a better way to get the geometry than cutting it.
If your job is thin, simple, high volume, and made of standard steel, price it both ways and let the numbers decide.
Common Questions About When to Use Water Jet Cutting
Does water jet cutting warp parts?
Not from heat, since none is introduced. That is one of the main reasons flat parts with tight flatness requirements are cut this way.
Will the cut edge need finishing?
Often not. The edge comes off matte with minimal burr. Whether it needs further work depends on the appearance standard the finished part has to meet.
Can water jet cut material that is already painted or coated?
Generally yes, since there is no heat to burn or blister a coating. Tell us about the coating when you request a quote so it factors into setup.
How do I know if my part is a water jet job?
Send the drawing with material, thickness, quantity, and any heat treatment or coating noted. Those details make the process choice obvious quickly.
Have a Part That Cannot Take Heat?
Send us your drawing or DXF, and we’ll follow up with a clear quote for water jet cutting, fast.

Laser Cutting vs. Water Jet Cutting: Which Process Fits Your Project?
Laser cutting vs water jet cutting is decided by heat more often than by anything else. A laser melts and blows material away, which is fast and precise but leaves a heat-affected zone along the cut. A water jet cuts cold, using pressurized water and abrasive, so the material next to the cut is unchanged. If your part cannot tolerate heat, the decision is already made. If it can, then thickness, edge finish, material type, and cost per part sort out the rest.
Does Laser Cutting vs Water Jet Cutting Come Down to Heat?
For a large share of jobs, yes. Laser cutting works by melting a narrow line through the material, which leaves a thin band along the edge where the metal was heated and cooled quickly. On most parts that band is irrelevant. On hardened or heat-treated material, on parts with tight requirements near the cut edge, and on some plastics and composites, it is not.
Water jet cutting removes material by erosion instead of melting, so nothing near the cut changes temper, hardness, or structure. That is the entire reason the process exists alongside laser rather than being replaced by it.
Water jet cutting removes material by erosion instead of melting, so nothing near the cut changes temper, hardness, or structure. That is the entire reason the process exists alongside laser rather than being replaced by it.
What Is the Difference in Edge Quality?
A laser edge on thin sheet is clean, square, and often ready to use as-is. As thickness increases, laser edges pick up more taper and dross, and secondary finishing becomes more likely.
A water jet edge comes off with a slightly matte, sandblasted texture and no burr worth mentioning. It stays consistent as thickness increases, though the cut can taper slightly on thicker material unless the machine compensates for it.
Which Process Handles Thicker Material?
Water jet, generally. Laser cutting is most efficient on thinner sheet and loses speed and edge quality as material gets thicker. Water jet cutting keeps working through much heavier plate, just more slowly. For thick stainless or aluminum plate, water jet is often the practical answer even when a laser could technically make the cut.
What Materials Can Each Process Cut?
Laser cutting is a metal process for most shops, and it handles reflective materials like aluminum and copper less readily than steel. Water jet cutting is close to material-agnostic. Metal, stone, glass, composite, rubber, and foam all cut on the same machine, which matters when a job involves something other than sheet metal.
For stainless specifically, both processes are used routinely, and the choice usually turns on thickness and whether the edge will be visible or further worked.
Which Is Faster and Cheaper Per Part?
On thin sheet in volume, laser cutting is generally faster and cheaper per part, and the gap widens as quantity climbs. Water jet runs slower and carries abrasive cost, which shows up on high-volume thin-gauge work.
That comparison flips on thick material, on parts that would need deburring or heat-affected material removed after lasering, and on short runs where setup dominates. Cost per part is the number to compare, not cost per hour.
How Precise Is Each Process?
Both are precise enough for the vast majority of fabricated parts. Laser holds a very narrow kerf, which helps on fine detail, small holes, and tight nesting. Water jet holds close tolerances too, with kerf width and taper as the factors to account for on intricate geometry. Neither is a limitation on typical fabrication work.
Which Process Fits Your Project?
Thin Sheet in Production Volume?
Laser, in most cases. Speed and cost per part favor it clearly, and edge quality on thin material is excellent straight off the machine.
Thick Plate or Heavy Profiles?
Water jet. It keeps a consistent edge through heavier material where laser performance falls off.
Heat-Sensitive or Hardened Material?
Water jet, without much debate. Cutting cold is the whole point, and it protects temper and hardness right up to the edge.
Non-Metal or Mixed-Material Jobs?
Water jet. Being able to cut stone, glass, composite, and metal on one machine consolidates jobs that would otherwise need two processes.
Common Questions About Laser Cutting vs Water Jet Cutting
Can one part use both processes?
Yes, and it happens on jobs where different features have different requirements. There is no rule that a single part has to be cut entirely one way.
Does the heat-affected zone actually matter on ordinary steel parts?
Usually not. It becomes a factor on hardened or heat-treated material, on parts with critical properties near the cut, and where a subsequent operation is sensitive to the condition of the edge.
Which one gives a better edge for a visible finished surface?
It depends on the look you want. A laser edge on thin material is crisp and square. A water jet edge is matte and uniform. Both can be finished further if the appearance has to match a specific standard.
How do I know which one my job needs?
Send the drawing along with the material, thickness, quantity, and anything the part has to survive afterward. Those four details settle it faster than a general comparison can.
Have a Part to Cut?
Send us your drawing or DXF, and we’ll follow up with a clear quote and the process that fits, fast.